Choosing a Lamination Method
If you're choosing between hand lay-up, spray lay-up and Resin Transfer Moulding (RTM) for a GRP (glass reinforced plastic) part, the right process depends on production volume, part complexity, the finish you need, and budget. Below is a breakdown of each method, a diagram of the RTM process, a detailed comparison table, and a look at where injection moulding fits, and where it doesn't.
Hand Lay-Up, Explained
Hand lay-up is the most established fibreglass lamination method. Gelcoat is applied to an open mould, then fibreglass mat is placed by hand and wetted with resin, rollered to remove air, and built up in layers to the required thickness.
It suits low-volume runs, prototypes and large or complex one-off parts well, since tooling is simple and low cost. The trade-off is that it's labour-intensive.
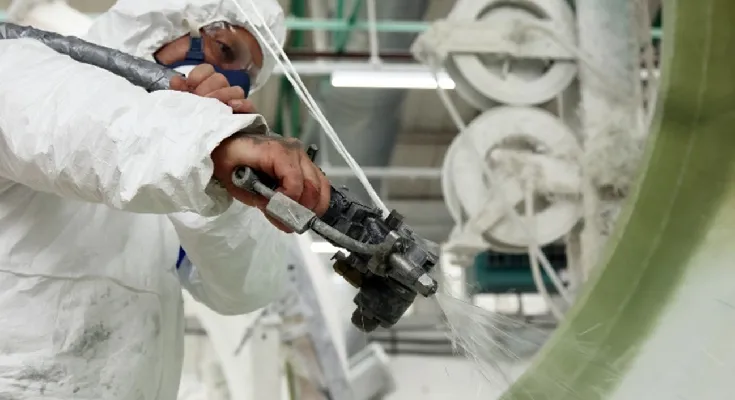
Spray Lay-Up, Explained
Spray lay-up uses a chopper gun to apply resin and chopped glass fibre together onto an open mould, once the gelcoat has cured. It's generally faster than hand lay-up and suits medium-volume runs or larger, more open shapes. The trade-off is less control over the thickness, so consistency depends on a skilled operator and good extraction equipment. It can also use more resin than hand lay-up, adding weight to the finished part.
Resin Transfer Moulding (RTM), Explained
RTM is a closed-mould process. The glass fibre mat is placed on either or both mould halves, and then a vacuum is applied to keep the moulds closed. Resin is injected via an injection machine, until it fully wets the mat. The part is then left to cure before being demoulded.
Because both mould faces are finished, RTM produces two smooth surfaces rather than one, with tighter thickness control than open moulding.1 Tooling costs more than hand or spray lay, since two matched mould halves are needed, but the process suits parts where consistency and finish matter most.
RTM Has Variants Worth Knowing
"RTM" covers more than one approach. Traditional RTM uses a matched, steel-backed mould set. Lighter variants, sometimes called RTM-Lite or Flex RTM, use a lighter male mould and vacuum assistance to draw resin in, reducing tooling weight and cost. Quantum's own process, RTM Lite, sits in this lighter-tooling category, giving many of RTM's consistency and finish benefits without the cost of full matched steel tooling.2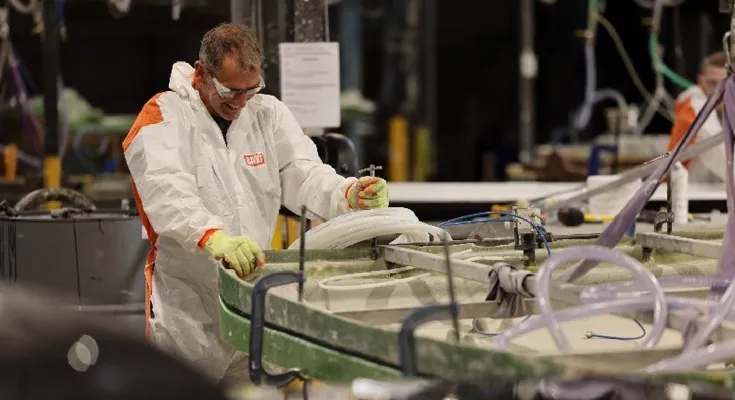
Comparing the Three GRP Methods Side by Side
The table below sets out how hand lay-up, spray lay-up and RTM compare across the factors that usually decide a process choice.
|
Criteria |
Hand Lay-Up |
Spray Lay-Up |
RTM (incl. RTM Lite) |
|
Mould type |
Open, single-sided |
Open, single-sided |
Closed, two-part mould |
|
Typical production volume |
Low (one-offs to small runs) |
Low to medium |
Low to medium, scalable with automation |
|
Part complexity suited |
Complex shapes, large parts |
Larger, more open shapes |
Complex shapes, but no deep undercuts |
|
Finished surfaces |
One side gel finished (mould side); other side typically textured |
One side gel finished (mould side); other side typically textured |
One side gel finished (mould side); other side also smooth. Can have gel on both surfaces |
|
Typical tooling cost |
Low |
Low |
Medium to high (two matched mould halves) |
|
Relative cycle time |
Slowest; labour-paced |
Faster than hand lay-up |
Can be fast, especially with heated or automated tooling3 |
|
Fibre orientation control |
Good (mat placed and rollered by hand) |
Lower (chopped fibre sprayed at random orientation) |
Good (reinforcement positioned before injection) |
|
Thickness consistency |
Good with a skilled operator |
Good but more operator-dependent |
High; closed mould controls thickness more accurately |
|
Operator skill dependency |
High |
High (equipment plus technique) |
Lower once the process is set up |
|
Emissions / H&S notes |
Styrene exposure during hand wet-out; standard extraction5 |
Higher airborne exposure from spraying; needs strong extraction and PPE |
Lower emissions; resin contained within closed mould |
|
Best suited for |
Prototypes, one-offs, large or highly complex parts |
Medium-volume, large or open parts needing speed |
Parts needing two-sided finish, consistency or repeat production runs |
Making the Right Choice for Your Part
The right process depends on your part more than any general rule: how many you need, how complex the shape is, what finish matters, and what you can spend on tooling. Quantum can talk through hand lay, spray lay and RTM Lite options for a specific part and help decide which fits best before tooling begins.
FAQ
What is RTM in composite manufacturing?
RTM (Resin Transfer Moulding) is a closed-mould process where resin is injected into a mould containing pre-placed fibre reinforcement, giving two finished surfaces and tighter thickness control than open moulding methods.
Is spray lay-up faster than hand lay-up?
Generally yes, spray lay-up can be quicker for larger, simpler shapes, though it offers less control over fibre orientation and thickness than hand lay-up.
Can GRP parts be made using injection moulding?
Not typically. Injection moulding usually applies to thermoplastics at high volume, while GRP lamination methods (hand lay, spray lay, RTM) use thermoset resin and fibre reinforcement, suiting different parts and volumes.
Resources
- CSIR – National Aerospace Laboratories (2021) Resin Transfer Moulding Processes. Bangalore: NAL. Available at: [https://www.nal.res.in/en/techniques/resin-transfer-moulding-processes] (Accessed: 24 September 2026).
- Rudd, C.D., Long, A.C., Kendall, K.N. and Mangin, C.G.E. (1997) Liquid moulding technologies: resin transfer moulding, structural reaction injection moulding and related processing techniques. Cambridge: Woodhead Publishing. Available at: [https://api.pageplace.de/preview/DT0400.9781845695446_A24169061/preview-9781845695446_A24169061.pdf] (Accessed: 24 September 2026).
- Advani, S.G. and Hsiao, K.-T. (eds.) (2012) Manufacturing techniques for polymer matrix composites (PMCs). Cambridge: Woodhead Publishing. Referenced via: 'Resin Transfer Molding Process — an overview', ScienceDirect Topics. Available at: [https://www.sciencedirect.com/topics/engineering/resin-transfer-molding-process] (Accessed: 24 September 2026).
- Nasir, S.S., Ariffin, A.K. and Ihsan, A.K.A.M. (2018) 'Effects of gelcoat thickness on mechanical properties of woven glass/polyester laminated composite', International Journal of Mechanical Engineering and Technology, 9(4), pp. 1088–1096. Available at: [https://www.researchgate.net/publication/325221510_Effects_of_gelcoat_thickness_on_mechanical_properties_of_woven_glasspolyester_laminated_composite] (Accessed: 24 September 2026).
- Health and Safety Executive (2019) EH40/2005 Workplace exposure limits. 4th edn. London: HSE. Available at: [https://www.hse.gov.uk/pubns/priced/eh40.pdf].